Recycling plastic and the processing choices that make it work
Why recycling plastic is still a processing challenge
Recycling plastic works when products are designed for collection, sorted into clean material streams, processed with controlled heat and filtration, and sold into end markets that can use the recycled resin consistently. The technical route is familiar, but the system is uneven. The OECD’s Global Plastics Outlook reported that only about 9% of global plastic waste was ultimately recycled in 2019 after recycling losses. Eurostat reported that the EU recycled 41% of generated plastic packaging waste in 2022. In the United States, EPA municipal waste data for 2018 put the recycling rate for plastic containers and packaging at 13.6%. For plastics processors, the limiting factor is often not whether a polymer can melt. It is whether the item can be collected, identified, cleaned, separated and reused without losing too much value.
For manufacturers, converters and packaging designers, the practical question is not only “Is this plastic recyclable?” A more useful question is: “Can this item move through the recycling system available in its market and come back as material with predictable performance?” That is where plastic processing choices become decisive.
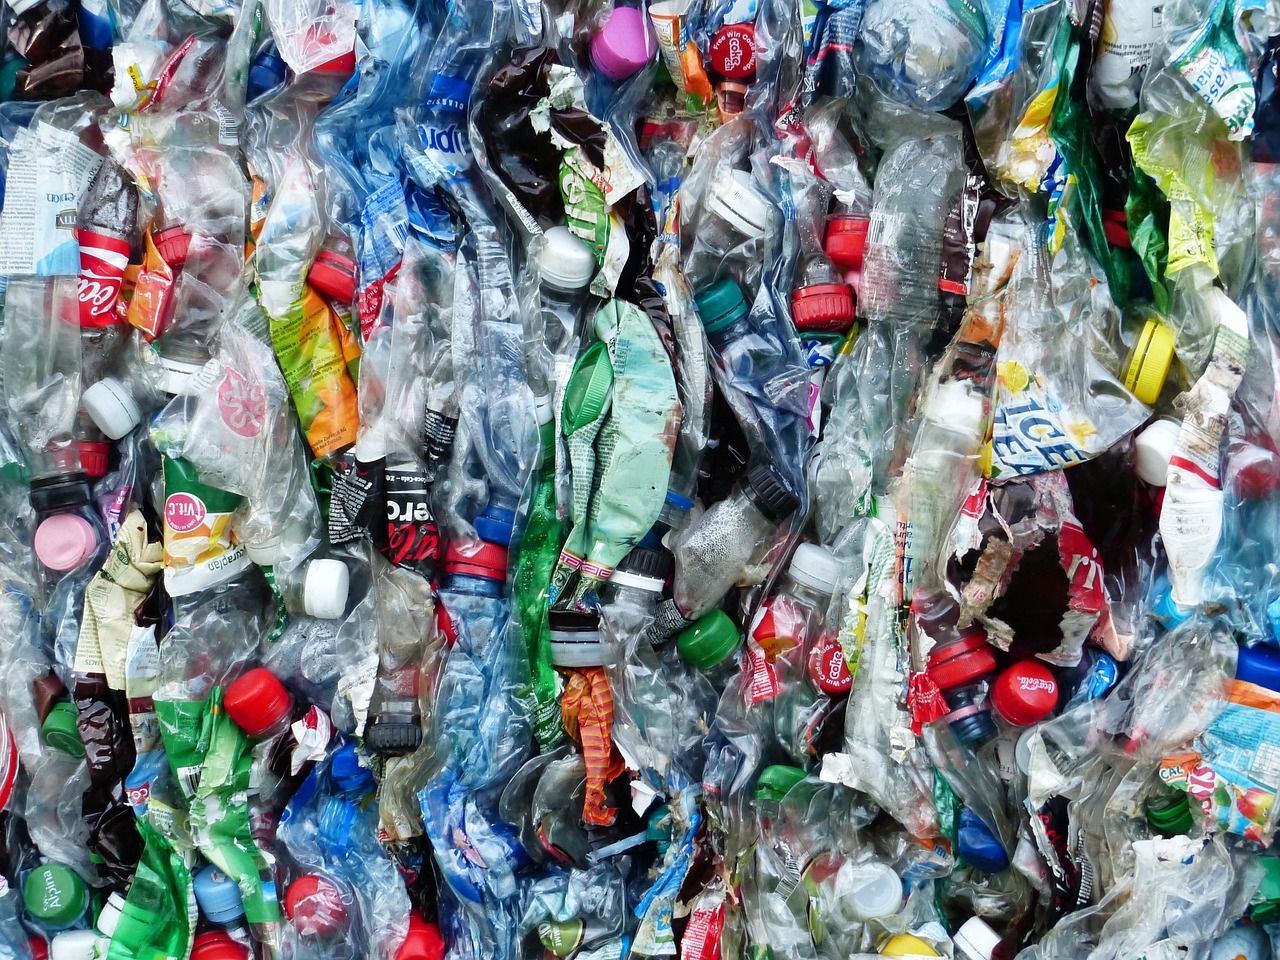
How the recycling chain turns plastic waste into resin
Most plastic recycling used for packaging and consumer products is mechanical recycling. This route keeps the polymer largely intact. Chemical processes, by contrast, break polymers or mixed plastic streams into smaller molecules, oils or monomers. Mechanical recycling remains widely used because it is commercially established, relatively direct and suitable for common streams such as PET bottles, HDPE containers and selected PP packaging.
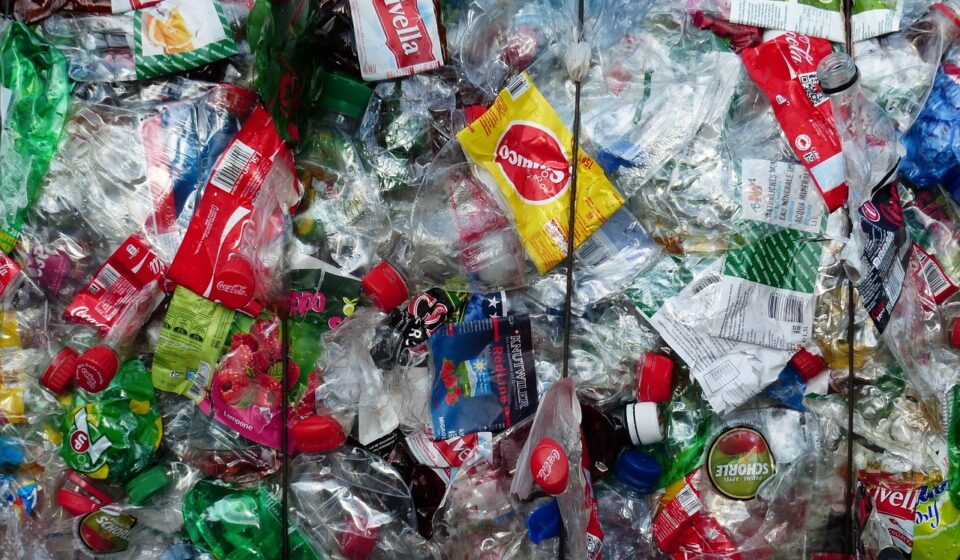
A typical mechanical recycling chain starts with collection from households, businesses, deposit systems or industrial scrap. The material is then sorted by polymer, color, shape and sometimes food-contact history. Labels, closures, dirt, organic residues and incompatible materials must be removed. After that, the plastic is size-reduced into flakes, washed, dried and processed through extrusion with melt filtration. The recycled material is then pelletized, compounded or converted directly into sheet, fiber, bottles, pipe, crates, pallets, film or molded goods.
Each stage removes contamination, but it can also remove value. A bale of clear PET bottles can become high-value rPET if color, PVC, multilayer materials and food residue are controlled. A mixed flexible packaging stream usually has less value because PE, PP, adhesives, inks and barrier layers are harder to separate. This is why recycling rates can be stronger for certain formats than for the plastics market as a whole. NAPCOR’s 2024 PET Recycling Report, released in December 2025, reported a 30.2% U.S. PET bottle recycling rate for 2024, down from 32.5% in 2023 but still above its 10-year average. PET bottles are not a perfect system, but they show how standard formats, identification and reliable end markets support recovery.
Material choices that improve recyclability
Recycling plastic starts at the design table. The resin, colorant, barrier system, adhesive, label, closure and decoration all affect whether a recycler can identify and process the item. A package may look simple to a consumer but still create problems at a material recovery facility if it uses a full-body shrink sleeve that blocks near-infrared detection, contains a black pigment that optical sorters cannot read, or combines incompatible layers that cannot be economically separated.
Design for recycling does not mean every product must use one material in every case. It means the designer should understand the dominant recycling stream and avoid features that reduce yield, contaminate output or create processing defects. For rigid packaging, mono-material structures are usually easier to handle. For flexible packaging, the challenge is greater because performance often depends on seal layers, barrier films, tie layers and printed surfaces.
| Design choice | Effect on recycling plastic | Practical direction |
|---|---|---|
| Clear or light-colored PET | Maintains more options for bottle-to-bottle, sheet and fiber markets | Use color only when needed for product protection or brand requirements |
| Natural HDPE | Often retains higher value than heavily pigmented HDPE | Keep pigments, labels and closures compatible with the HDPE stream |
| Mono-material PE or PP flexible packaging | Improves the chance of recovery compared with mixed-material laminates | Balance barrier needs with structures that can enter recognized PE or PP streams |
| Full-body shrink sleeves | May interfere with optical sorting and washing if not designed correctly | Use washable, perforated or recyclable sleeve systems matched to the base container |
| Dark carbon-black colorants | Can reduce detectability in some near-infrared sorting systems | Consider detectable black or alternative colors where recycling claims matter |
| Permanent adhesives and incompatible labels | Can create residue, discoloration and gel defects during extrusion | Choose adhesives and labels tested for the target recycling stream |
The Association of Plastic Recyclers Design Guide and similar regional design protocols are often used by packaging teams because they connect design choices with recycler acceptance. For processors, the key point is that recyclability is not defined only by a resin code. A PET bottle, PP tub or HDPE closure can still fail in recycling if the full package design is incompatible with sorting, washing or remelting.
What policy is changing for plastics processors
Policy is increasingly turning recycling plastic from a voluntary sustainability claim into a measurable compliance issue. In the European Union, Regulation (EU) 2025/40 on packaging and packaging waste entered into force on February 11, 2025, and began applying on a phased basis from August 12, 2026. European Commission materials describe the regulation as a move toward less waste, more recycling, safer food-contact packaging and greater use of recycled plastic in new plastic packaging. Requirements related to recyclability, recycled content, reuse, labelling and packaging minimization phase in over different dates, with major 2030 and 2040 milestones.
For companies supplying packaging into EU markets, documentation is becoming more important. A processor may need to know the polymer family, recycled content source, food-contact status, additives, inks, packaging weight and evidence that the format can be recycled under defined criteria. The regulation also links future compliance to practical recyclability, not just a theoretical statement that a polymer can be recycled somewhere.
International trade rules also matter. The Basel Convention’s plastic waste amendments have applied since January 1, 2021, bringing many mixed or contaminated plastic waste shipments under prior informed consent procedures. This has made the quality and traceability of exported plastic waste more important. For recyclers and traders, low-contamination, well-sorted streams are easier to move and process responsibly than mixed bales with uncertain composition.
In the United States, national municipal waste data show how difficult the plastics stream remains. EPA’s 2018 data reported that PET bottles and jars had a 29.1% recycling rate, natural HDPE bottles had a 29.3% recycling rate, and overall plastic containers and packaging reached 13.6%. Since then, policy activity has continued at state and local levels, including extended producer responsibility, deposit return and recycled-content rules in some jurisdictions. The practical implication is clear: processors should expect more requests for verified recycled content, design-for-recycling evidence and chain-of-custody data.
Quality limits that determine where recycled resin can be used
Recycled resin is not automatically equal to virgin resin in every application. Its value depends on polymer degradation, contamination, odor, color, melt flow, intrinsic viscosity, moisture level and regulatory status. PET used for beverage bottles, for example, needs tight control of intrinsic viscosity, acetaldehyde, color and food-contact safety. PP used in injection molding may tolerate more color variation, but it still needs stable melt flow and low contamination to avoid brittle parts or surface defects.
Thermal history is a major issue. Every melt cycle can shorten polymer chains or change rheology if processing is not controlled. Moisture can hydrolyze PET. PVC contamination in PET can cause discoloration and degradation at PET processing temperatures. Small amounts of incompatible polymers can create gels, black specks, weak weld lines or poor film appearance. For these reasons, washing, drying, melt filtration and quality testing are not optional steps; they are part of the product specification.
Food-contact applications add another layer. Recycled plastic for food packaging usually needs an approved process, controlled input materials and evidence that contaminants are removed to safe levels. This is one reason recycled resin may be used first in non-food packaging, textiles, strapping, drainage products, construction materials, automotive parts or reusable crates. Higher-value circular uses are possible, but they require tighter feedstock control and more investment in processing technology. See also: Buying Guides.
Economics can be just as important as engineering. Recyclers need enough clean material to run equipment efficiently. Buyers need recycled resin that performs consistently. When virgin resin prices fall, recycled resin can struggle unless regulation, brand commitments or customer specifications maintain demand. Recycling plastic therefore depends on both technical capability and market pull.
Mechanical recycling, advanced recycling and realistic expectations
Mechanical recycling should remain the first option for clean, sortable and compatible streams because it preserves material value with fewer process steps. It is well suited to PET bottles, natural HDPE containers, selected PP rigid packaging and clean industrial scrap. It is less effective for heavily contaminated waste, multilayer barrier packaging, complex flexible films and plastics mixed with non-plastic materials.
Advanced or chemical recycling is often discussed as a complementary route. Depending on the technology, it may include depolymerization, purification, solvolysis, gasification or pyrolysis. These methods can sometimes handle streams that are difficult for mechanical recycling, but they are not interchangeable with a conventional wash-and-extrude line. They vary widely in energy use, output quality, yield, emissions control, regulation and whether the output is used as new plastic feedstock or as fuel-like material.
The more practical approach is to match the recycling route to the stream. Clean PET bottles should not be treated the same way as contaminated mixed polyolefin film. Industrial PP scrap from a molding plant should not be treated the same way as post-consumer multilayer snack packaging. A workable recycling strategy starts with prevention and redesign, then reuse where appropriate, then high-yield mechanical recycling, and then other technologies for streams that cannot be handled effectively by mechanical systems.
A practical checklist for manufacturers and converters
Companies that want packaging or products to perform better in recycling can act before material reaches a recycler. The following checklist focuses on steps that are visible to processors, converters and brand owners.
- Define the target recycling stream early. Design for the actual collection and sorting system in the sales market, not for a theoretical system.
- Choose compatible materials. Avoid unnecessary multilayer structures, incompatible closures, difficult labels and additives that reduce recyclate quality.
- Minimize color and decoration risk. Dark pigments, metallic effects, heavy printing and permanent adhesives can reduce value if not tested.
- Control industrial scrap separately. Clean in-plant scrap is often easier to recycle than post-consumer material and should not be mixed with lower-quality waste.
- Specify recycled content carefully. Include polymer type, PCR or PIR status, food-contact requirements, melt flow or viscosity, color range and contamination limits.
- Test at processing scale. Laboratory results are useful, but extrusion, thermoforming, injection molding, blow molding or film trials reveal real performance limits.
- Keep documentation. Regulations and customers increasingly ask for proof of recycled content, origin, mass balance, safety and recyclability.
The main lesson is that recycling plastic is not a single downstream event. It is the result of decisions made across product design, resin selection, conversion, consumer use, collection, sorting, washing, extrusion and purchasing.
Frequently asked questions
Which plastics are usually easier to recycle?
PET bottles, natural HDPE bottles and clean industrial scrap are often easier to recycle because they can be collected in recognizable streams and have established end markets. PP rigid packaging and PE films can also be recycled where appropriate collection and sorting systems exist, but acceptance varies by market and format.
Why can two packages with the same resin code have different recyclability?
The resin code identifies the main polymer family, but recyclability also depends on color, labels, adhesives, barriers, closures, additives and local recycling infrastructure. A clear PET bottle and a multilayer PET-containing package may behave very differently in sorting and reprocessing.
Is recycled plastic always lower quality?
No. Recycled plastic can perform well when the feedstock is clean, sorted and processed under controlled conditions. However, recycled resin can have more variation than virgin resin, so applications must be matched to the material’s tested properties and regulatory status.
Is biodegradable plastic the same as recyclable plastic?
No. Biodegradable or compostable plastics are designed for specific degradation conditions, not necessarily for mechanical recycling. If they enter the wrong recycling stream, they may contaminate conventional recycled resin. Clear labelling and separate treatment routes are important.
What is the biggest opportunity for improving plastic recycling?
The biggest opportunity is aligning product design with real recycling infrastructure. Better collection helps, but recyclers also need packages that can be identified, separated, cleaned and remelted into resin that buyers trust. That requires cooperation between designers, resin suppliers, converters, brands, waste managers and recyclers.