Plastic processing explained for material selection and manufacturing control
What plastic processing means in manufacturing
Plastic processing covers the manufacturing methods used to convert polymer resin, additives, fillers and, in some cases, recycled feedstock into parts, sheets, films, tubes, profiles or finished products. The basic sequence is usually familiar: prepare the material, heat or otherwise condition it, shape it in a mold, die or tool, cool or cure it, then inspect and finish the part. The commercial decision is more complex. A good plastic processing plan has to match resin behavior, part geometry, production volume, tolerance, surface quality, safety requirements and end-of-life expectations.
For manufacturers and sourcing teams, the key question is not simply which process is considered best. It is which process can repeatedly produce the required part at the right cost, with acceptable scrap, documented quality and realistic material availability. That makes process selection a cross-functional decision for design, material engineering, tooling, operations, purchasing and quality teams.
The main plastic processing routes and where they fit
Most industrial plastic processing methods fall into a few major families. They differ in how the polymer is shaped, how the tooling is built, and how much freedom the designer has over wall thickness, dimensional precision and production speed.
| Process | Typical outputs | Where it fits well | Common limitations |
|---|---|---|---|
| Injection molding | Housings, caps, connectors, gears, medical and consumer parts | High-volume three-dimensional parts with repeatable features | High mold cost, shrinkage, weld lines and long tooling lead times |
| Extrusion | Pipe, tube, sheet, film, profiles and cable coating | Continuous products with a constant cross-section or controlled film structure | Die design, thickness control, cooling uniformity and downstream handling are critical |
| Blow molding | Bottles, containers, tanks and ducts | Hollow parts where weight and wall distribution matter | Parison control, pinch-off quality and recycled-content consistency can be difficult |
| Thermoforming | Trays, clamshells, panels and packaging inserts | Large or thin-wall shapes with lower tooling cost than injection molding | Wall thinning, trimming scrap and limited detail compared with molding |
| Compression and transfer molding | Thermoset parts, composites and high-strength components | Materials that cure under heat and pressure or need fiber reinforcement | Cycle time, flash control and post-cure requirements |
| Rotational molding | Large hollow tanks, bins, playground parts and housings | Large, stress-relieved hollow parts with relatively low tooling pressure | Long cycles, limited fine detail and material selection constraints |
| Additive manufacturing | Prototypes, jigs, low-volume parts and complex geometries | Fast iteration and shapes that are difficult to tool conventionally | Build speed, anisotropy, surface finish and qualification requirements |
Additive manufacturing is now part of many plastic processing discussions, but it should not be treated as a direct replacement for molding or extrusion in every application. ISO lists standards for additive manufacturing processes, materials and equipment, including material extrusion-based additive manufacturing of plastic materials. That reflects the need for controlled terminology, qualification and data handling as 3D-printed polymer parts move into more demanding uses. (iso.org)
Material choice sets the process window
The selected resin determines how forgiving the process will be. Thermoplastics such as PE, PP, PVC, PET, ABS, nylon and engineering resins soften when heated and can often be remelted. Thermosets and many reactive systems cure into a crosslinked structure, so processing depends on heat, pressure and cure chemistry rather than simple remelting. Amorphous polymers also behave differently from semi-crystalline polymers during cooling, shrinkage and transparency control.
Material preparation is often where quality is won or lost. Hygroscopic materials may need controlled drying before molding or extrusion. Filled and glass-reinforced grades can improve stiffness, but they may also increase tool wear and change flow behavior. Colorants, flame retardants, impact modifiers, slip agents and stabilizers can affect processing temperature, screw recovery, venting, surface appearance and weld-line strength. A melt flow value is useful, but it is not a complete process recipe.
Recent resin data also show why processors monitor supply as closely as machine settings. American Chemistry Council year-end resin statistics published in March 2026 reported 136.123 billion pounds of total plastics production in 2025, up 0.1% from 2024, and 138.130 billion pounds of total sales and captive use, up 1.3%. The same table showed total thermoplastics production nearly flat at 118.729 billion pounds, while thermoplastics sales and captive use rose 1.6%. (americanchemistry.com)
Regional differences matter as well. Plastics Europe’s 2025 Fast Facts report presented preliminary 2024 figures showing European plastics production at 54.6 million tonnes and a 15.4% circular plastics share in production under its stated definition. That type of data does not tell an individual processor which resin to buy, but it does show that recycled, bio-based and chemically recycled streams are becoming part of mainstream material planning rather than a side topic. (amaplast.org)
Design and tooling decisions that prevent processing problems
Plastic parts should be designed for the process before the tool is cut. Uniform wall thickness, proper draft, generous radii, balanced flow paths, suitable gate location and realistic tolerances all reduce the risk of sink marks, warpage, incomplete filling and cosmetic defects. A part designed like a machined metal component may still be possible to mold, but it can become unnecessarily expensive or unstable in production.
Dimensional control in plastics depends on the combined behavior of material, part design, tool layout and processing conditions. ISO 20457 on plastics moulded parts addresses tolerances and acceptance conditions, and its introduction notes that plastic moulded parts cannot simply borrow metal tolerancing assumptions because plastics differ in stiffness, deformability and processing behavior. (iso.org)
Tooling choices also shape long-term cost. In injection molding, cooling-channel design can dominate cycle time and dimensional stability. In extrusion, die geometry and calibration control wall thickness, surface quality and line speed. In thermoforming, the sheet temperature window, plug assist, vacuum pattern and trimming strategy affect both part quality and scrap rate. In blow molding, parison programming or preform design has a direct effect on wall distribution and drop performance.
The practical lesson is to set tolerances around function, not habit. Critical interfaces may justify tighter dimensions and more inspection, while non-critical surfaces can often accept wider tolerances, texture variation or minor witness lines. Over-tolerancing plastic parts raises tooling cost, extends launch time and may increase rejection without improving the user experience.
Process control, testing and plant safety
Once production begins, stable plastic processing depends on controlling the variables that change melt history and part cooling. For molding, these variables include melt temperature, mold temperature, injection speed, packing pressure, hold time, cushion, screw recovery and cooling time. For extrusion, they include barrel profile, screw speed, melt pressure, die temperature, haul-off speed, cooling rate and line tension. For thermoforming, sheet temperature uniformity is often as important as forming pressure.
Quality systems should connect machine settings to measurable outcomes. Short shots, flash, voids, bubbles, burn marks, splay, gels, black specks, warpage and brittle failure can point to different combinations of material, tool, drying, temperature, pressure or handling causes. A useful control plan defines which variables are recorded, which tests are performed, and which defects trigger containment or process adjustment.
Standardized specimen preparation and testing help separate material behavior from processing noise. ISO 294-1 specifies general principles for injection moulding thermoplastic test specimens and aims to provide reproducible moulding conditions for reference data. ASTM D638 covers tensile testing of reinforced and unreinforced plastics under defined specimen, conditioning and test-speed conditions. (iso.org)
Safety is not separate from productivity. OSHA’s plastics machinery guidance notes that plastics processing machines can expose employees to nip points, moving parts, high voltage and high temperature, and its horizontal injection molding guidance highlights risks such as crushing, amputation, electric shock and burns from hot plastic or surfaces. A plant that treats guarding, lockout, ventilation, training and personal protective equipment as production fundamentals is less likely to lose capacity to preventable incidents. (osha.gov) See also: Buying Guides.
Sustainability and recycling pressure change process decisions
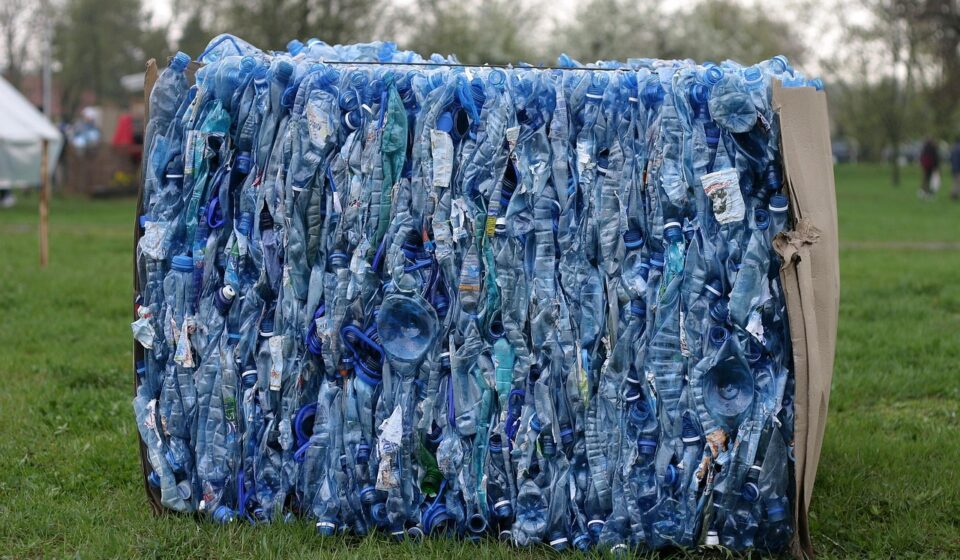
Recycling targets, customer specifications and procurement policies are changing how processors think about materials. Recycled resin can work well in many applications, but it may introduce variation in melt flow, moisture, odor, color, contamination, mechanical performance and regulatory status. The best results usually come from designing the product, tool and quality plan around the actual recycled stream rather than assuming it behaves like virgin resin.
The scale of the waste challenge explains why this matters. The U.S. EPA’s plastics material-specific data page, based on its 2018 municipal solid waste dataset, reported 35.7 million tons of plastics generation in the United States, equal to 12.2% of MSW generation. It also reported 3.09 million tons recycled, an 8.7% recycling rate, and 26.97 million tons landfilled in 2018. These are older data, but they remain a widely cited federal baseline for U.S. plastics in municipal solid waste. (epa.gov)
A 2024 National Institute of Standards and Technology report on the U.S. plastics recycling economy reviewed recycling programs, chemical recycling, stakeholders, incentives, barriers and challenges to increasing recycling and recycled-content use. For processors, the practical point is clear: circularity is not achieved only at the recycling plant. It is also influenced by resin selection, additive packages, product design, labeling, sorting compatibility, contamination control and the tolerance of the final application. (nist.gov)
In production, sustainability often starts with avoidable loss. Lower start-up scrap, better drying discipline, closed-loop regrind control, preventive maintenance, optimized cooling and more accurate trimming can reduce waste before any end-of-life claim is made. For film, sheet and thermoforming, trim recovery may be central to the economics. For injection molding, runners, purging and rejected parts need a clear segregation plan to prevent accidental mixing of incompatible materials.
A practical selection framework for engineers and buyers
When comparing plastic processing options, teams should work from requirements toward equipment, not from equipment toward requirements. The following questions help prevent early decisions from turning into expensive late-stage changes:
- What mechanical, thermal, chemical, electrical or appearance requirements must the part meet?
- Is the expected annual volume closer to prototype, bridge production, medium volume or mass production?
- Which dimensions are truly critical, and which can use wider plastic-appropriate tolerances?
- Will the part require virgin resin, recycled content, food-contact compliance, flame rating or outdoor stability?
- How much tooling investment and lead time are acceptable before first production parts?
- Can the design be modified to improve flow, cooling, wall uniformity, demolding or trimming yield?
- Which tests will prove that the part meets requirements after processing, aging or exposure?
- How will scrap, regrind, traceability and material changes be controlled during production?
A simple rule helps keep the discussion grounded: choose injection molding when complex high-volume geometry justifies tooling; choose extrusion for continuous profiles, films, sheets or tubes; choose blow molding for hollow containers; choose thermoforming for shaped sheet products where tooling cost and speed matter; and choose additive manufacturing when design iteration, customization or low volume outweigh unit-cost limits. Exceptions exist, but this framework ties the decision to function and economics.
For sourcing teams, the most useful supplier conversations are specific. Instead of asking whether a processor can make plastic parts, ask which resin grades they have processed, what tolerances are realistic for the geometry, how they validate drying and melt quality, what defect history is typical for similar parts, and how they manage engineering changes. Those answers reveal more than a generic capability list.
Frequently asked questions
What is the difference between plastic processing and plastic manufacturing?
Plastic manufacturing is the broader industrial activity of producing plastic materials, components or finished goods. Plastic processing usually refers to the conversion step that shapes polymer materials into parts or forms, such as molding, extrusion, blow molding, thermoforming or additive manufacturing.
Which plastic processing method is most suitable for high-volume parts?
Injection molding is often selected for high-volume three-dimensional parts because cycle times can be short after tooling is built, and complex features can be formed repeatedly. However, extrusion may be more suitable for continuous products, and blow molding may be better for hollow packaging. The correct choice depends on geometry, volume, material and quality requirements.
Can recycled plastic be used in injection molding or extrusion?
Yes, recycled plastic can be used in many molding and extrusion applications when the feedstock is compatible, clean, tested and controlled. The processor may need to adjust drying, temperature, filtration, screw design, color control and inspection because recycled streams can vary more than virgin resin.
Why do plastic parts warp after processing?
Warpage usually comes from uneven shrinkage, unbalanced flow, non-uniform cooling, poor gate location, excessive orientation, unsuitable wall thickness or material variation. It is best addressed early through part design, mold design, cooling analysis and process validation rather than only by changing machine settings after launch.
How does 3D printing fit into plastic processing?
3D printing is a plastic processing route when polymer materials are built layer by layer into parts. It is valuable for prototypes, fixtures, customization and some low-volume production, but molded or extruded processes usually remain more economical for large volumes and demanding surface-finish requirements.